
MIG welding aluminum requires a compatible welder, a reliable way to feed aluminum wire, the correct shielding gas and careful preparation. A wire-feed machine intended only for gasless steel wire is not automatically suitable. Start with practice pieces of a known alloy and thickness before attempting a finished project.
Understanding MIG Welding and Aluminum
MIG uses a continuously fed electrode wire and an electric arc to join metal. For aluminum, the filler must be suitable for the base alloy. The wire becomes part of the joint; steel MIG wire does not produce a normal aluminum-to-aluminum weld.

Aluminum conducts heat readily and develops an oxide layer that must be removed before welding. Those properties, along with the difficulty of feeding soft wire, make preparation and equipment choice important. Do not use a melting-point figure as a welder setting: voltage, wire speed, thickness and travel speed work together.
Choose an Aluminum-Capable Welder and Feeding System
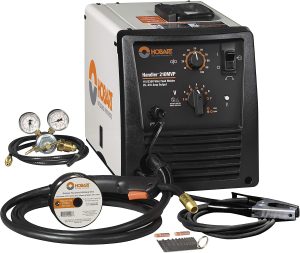
Hobart Handler 210MVP MIG Welder
- Model 500553 with 115/230 V input capability
- Up to 210 A output on 230 V input
- Accepts the optional SpoolRunner 100, part 300796
- Spool gun, aluminum wire and shielding-gas supply are separate requirements
The Handler 210MVP supports aluminum welding with the separately purchased SpoolRunner 100. The standard HR-100 MIG gun supplied with the welder is not that spool gun. Hobart’s model specification and welding chart identify the compatible accessory and starting settings.
Check the required circuit, plug and input voltage before buying. Available output differs on 115 V and 230 V, and the machine’s maximum amperage is not a continuous-duty rating. This package alone does not include every item needed for an aluminum project.

Spool guns keep the wire supply close to the torch, reducing the distance soft aluminum wire must travel. A compatible push-pull system is another option. Match the gun, liner, drive components and contact tip to the manufacturer’s approved wire size; a spool gun is not universally interchangeable between machines.
Prepare the Work Area and Protective Equipment
Use a stable, noncombustible welding surface and suitable clamps. Remove flammable materials, provide appropriate ventilation and keep people nearby protected from the arc. Read the machine and shielding-gas instructions, including cylinder securing and handling requirements.
Wear a welding helmet with the correct filter shade for the process and current, safety glasses underneath, suitable welding gloves and protective clothing. Clear safety glasses alone do not protect against welding arc radiation.
BISON LIFE Clear Safety Glasses, 12 Pack
- Clear protective eyewear for appropriate workshop tasks
- Wear under a suitable welding helmet when welding
- Not a welding filter or a substitute for arc protection

How to Weld Aluminum with a MIG Welder
1. Identify the Alloy and Choose the Filler
Use material with a known alloy designation. ER4043 and ER5356 are common aluminum fillers, but neither is a universal choice. Select filler using the base-alloy chart and the finished part’s strength, corrosion, service-temperature and appearance requirements. A welding supplier can help resolve an unknown application.
For practice, use clean coupons rather than structural parts. An aluminum truck toolbox illustrates a finished product, not a guarantee that its alloy or joints are suitable for a beginner repair.
2. Clean and Fit the Joint
Remove oil and dirt with a cleaner approved for the task and let the surface dry. Avoid chlorinated solvents around welding. Then remove oxide with a stainless-steel brush reserved for aluminum. A brass brush or a brush already used on steel is not the specified preparation tool.
Fit and clamp the pieces securely without forcing a large gap. Our sheet-metal cutting guide explains tool choices for preparing stock. Keep cutting debris away from the joint and do not treat a shop vacuum as a welding-fume extractor.

3. Set Up Gas, Polarity and Wire Feed
Use the shielding gas specified for the aluminum process; 100% argon is the usual choice for this type of work. A steel-welding argon/CO₂ blend is not a substitute. Set the flow according to the equipment instructions and protect the gas coverage from drafts.
For the Handler’s aluminum setup, Hobart specifies DCEP, or electrode positive, and aluminum wire with the optional spool gun. Follow the machine’s chart for the selected input voltage, alloy, wire diameter and thickness. Disconnect power before making gun or polarity changes as instructed in the manual.
4. Practice and Adjust on Matching Scrap
Make a test weld on scrap of the same alloy and thickness. Follow the specified torch position and keep a consistent travel speed. A modest push angle is normally used for aluminum MIG welding. If wire feeding becomes erratic, stop and check the approved feed components and tension rather than forcing the wire through.
Burn-through, soot, porosity or poor fusion require adjustment or further preparation. A smooth-looking bead does not by itself establish a sound structural weld. Thin aluminum may require a different process or more specialized equipment than an ordinary MIG setup.
Miller’s aluminum MIG guide covers preparation and technique. For filler selection, consult the alloy chart and the manufacturer’s recommendations rather than choosing solely by price.
Aluminum Welding Demonstration
The following video is a general aluminum-welding demonstration. Confirm the setup for your own welder and spool gun; another machine’s controls or settings may differ.

FAQs on Welding Aluminum
Can I weld aluminum with my wire-feed welder?
Only if the manufacturer supports an appropriate aluminum process and feeding arrangement. Confirm shielding-gas capability, output, polarity, wire sizes and compatible gun. A gasless steel-wire machine is not automatically aluminum-ready.
Can you weld aluminum with steel wire?
No, not for ordinary aluminum-to-aluminum MIG welding. Use an aluminum filler selected for the base alloy and application. Joining dissimilar metals requires a different, specifically qualified approach.
What kind of wire do you use to weld aluminum?
Common choices include ER4043 and ER5356 aluminum wire, but the correct filler depends on the base alloy and service requirements. Follow a filler-selection chart and use a diameter approved for the welder and feeding system.
For general workshop planning, see our power-tool guide and woodworking shop-vac guide. Neither replaces the dedicated welding equipment and ventilation needed for this task. More practical project guides are available at ThreeTwoHome.